| Process | Capacity | Materials |
|---|---|---|
| Hot hand drop forging | [F01], [F02] presses | Brass, steel |
| Pressure die casting | [F03], [F04] machines | Aluminum, zinc |
| Gravity casting | To [F16] | Aluminum, zinc |
| Investment casting | To [F16] | Brass, steel, stainless |
| Extrusion | [F05] | Aluminum, brass |
Forging
Forging is used to shape heated metal under high compressive force, producing strong and durable components.
We run [F02] friction screw presses from [F01], forging brass and steel. Parts come off near-net, which means less machining stock, a denser grain and better fatigue life than a bar-turned equivalent. Dies are cut in our own tool room, so a die change during development happens here rather than at a supplier.

Die Casting
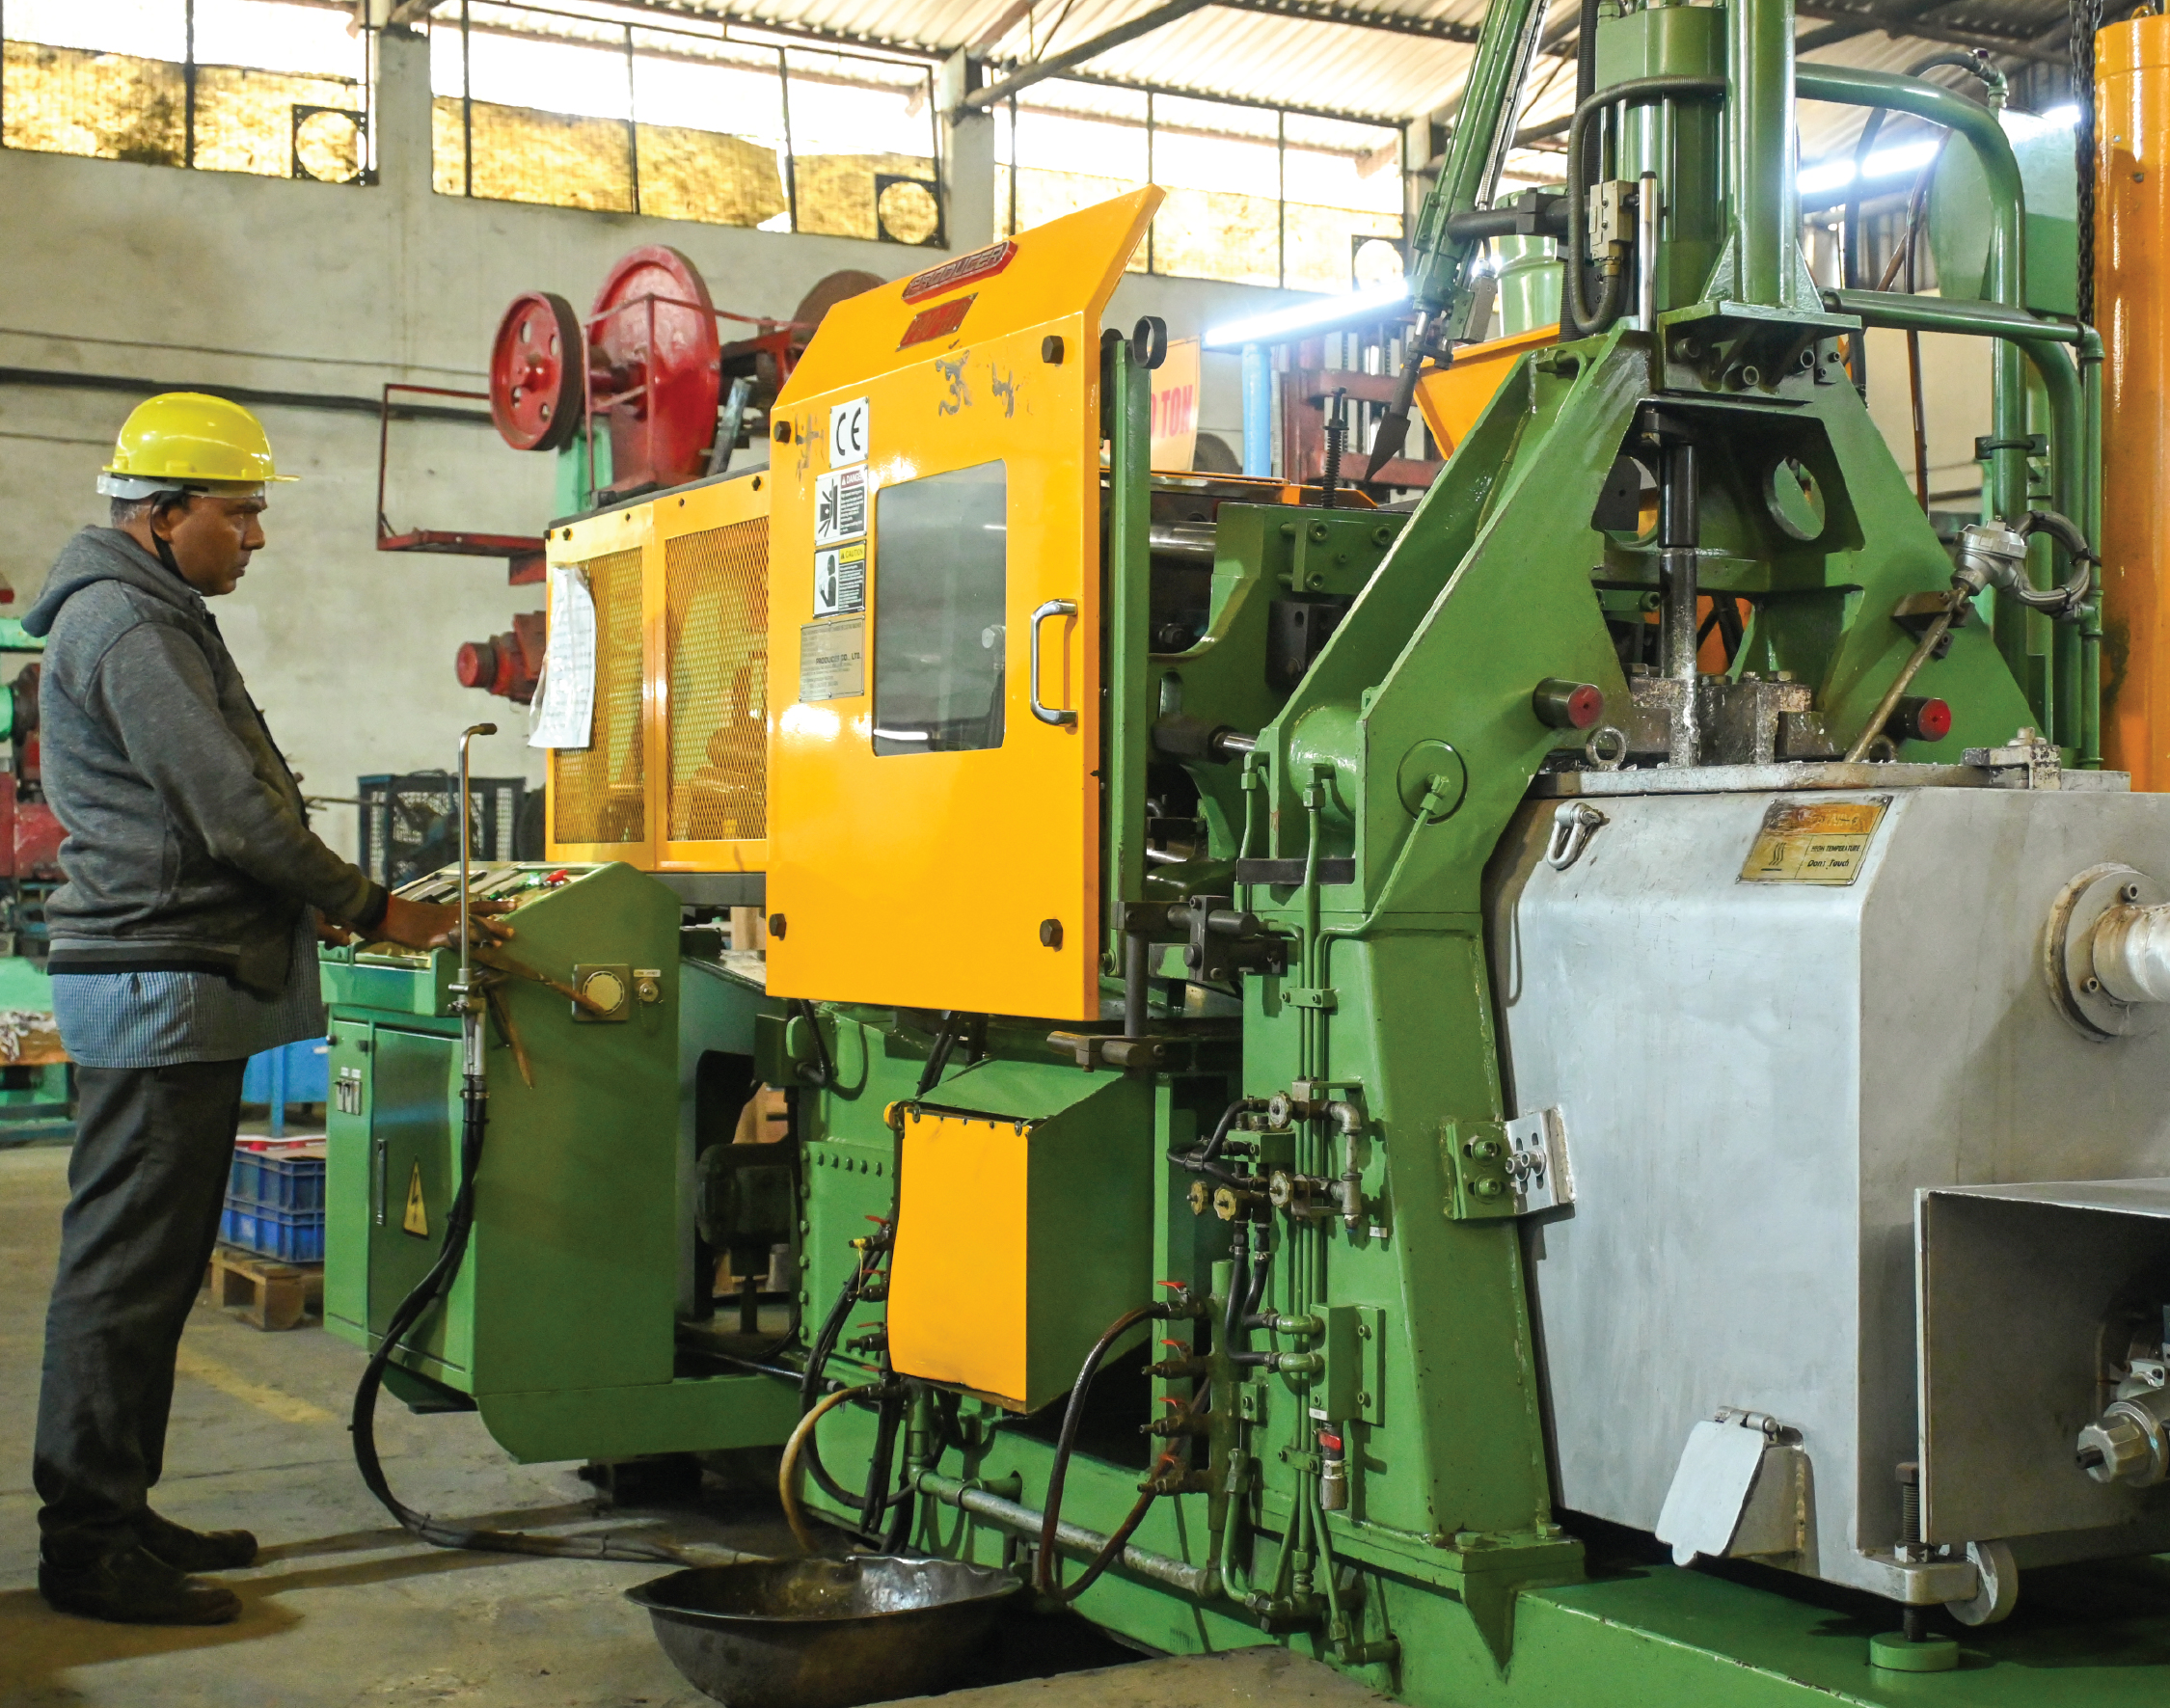
Die casting produces complex metal components by injecting molten metal into steel molds under high pressure.
[F04] machines from [F03], running aluminum and zinc. Molds are designed and cut in-house on VMC and EDM. Suited to volume parts where dimensional repeatability and surface finish both matter.
Extrusion
Extrusion forms metal profiles by forcing heated material through a shaped die.
Aluminum and brass profiles drawn to your section on our own automated line, press capacity [F05]. We develop the die, run the profile, then cut, machine and finish it in the same building. Die development takes about [F17].
.jpg)
Gravity Casting
Gravity casting is used to manufacture metal components by pouring molten metal into reusable molds under controlled conditions.
Used where a part needs a heavier section than pressure die casting will give, or where tooling cost has to stay low for a moderate volume. Good structural strength and a consistent surface straight from the mold.

Investment Casting (Lost Wax)
Investment casting is a precision casting process used to manufacture complex metal components with high dimensional accuracy and fine surface detail.
For geometry that cannot be die cast or machined economically. Maximum part weight [F16]. Frequently combined with machining on the same part, both done here.
.jpg)